Aluminum Investment Casting - A356 Precision Parts
Aluminum investment casting for complex A356 and C355 parts when geometry or volume does not suit HPDC. Compare investment cast aluminum vs die casting crossover volumes.
Production Capabilities
Supporting visuals for aluminum investment casting
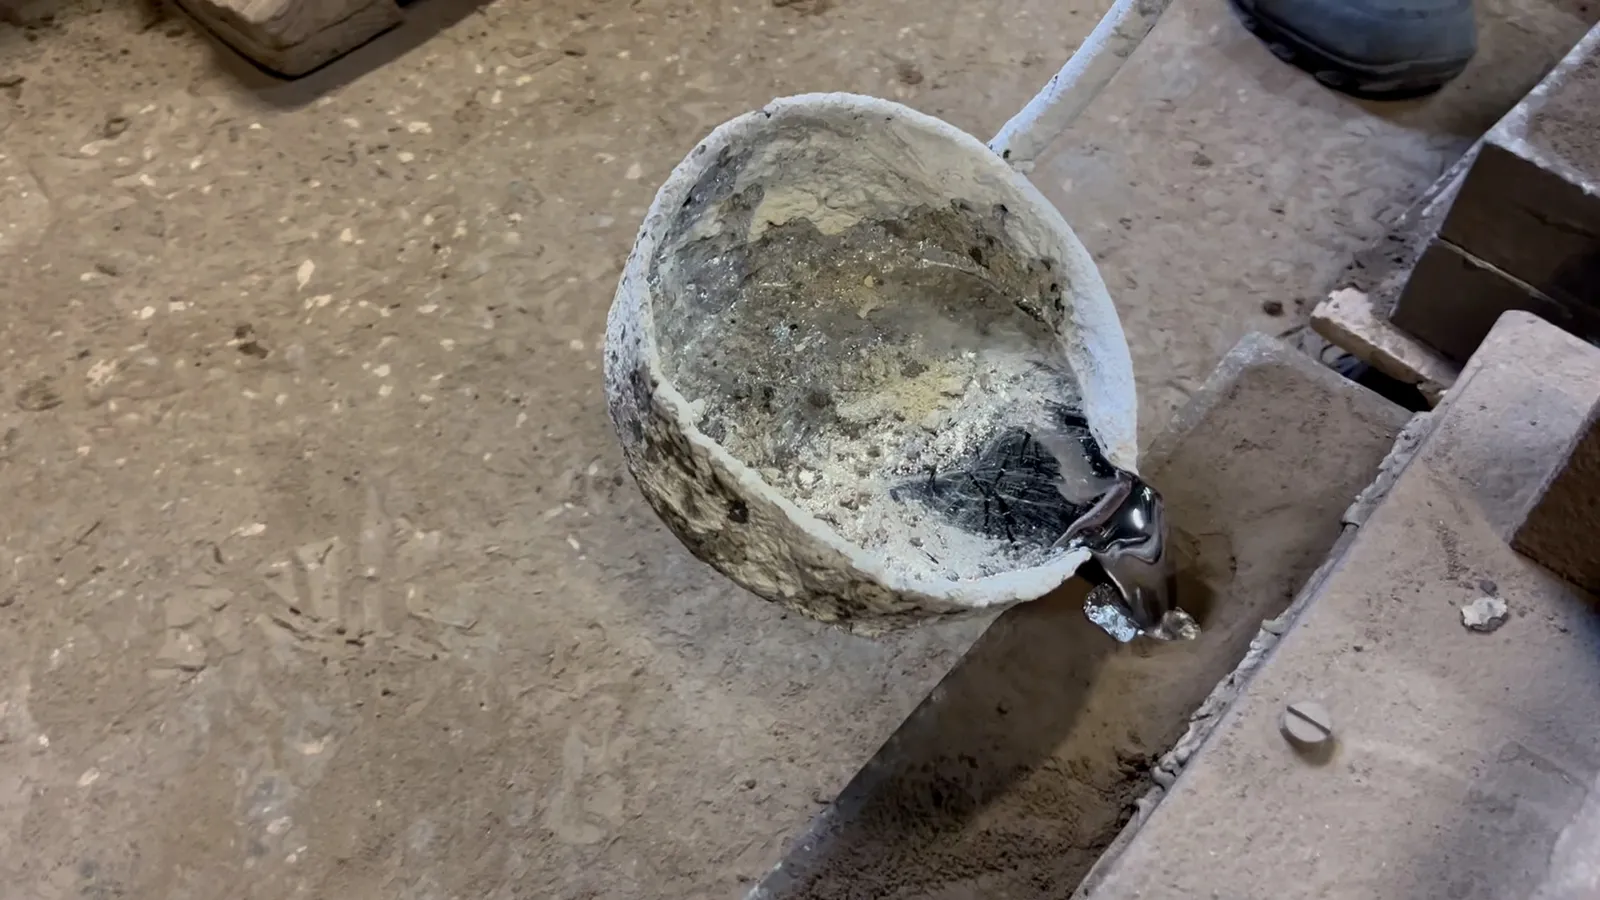
Manufacturing Operations
Die casting production, tooling fabrication, CNC machining, and quality inspection at our Nanjing facility.
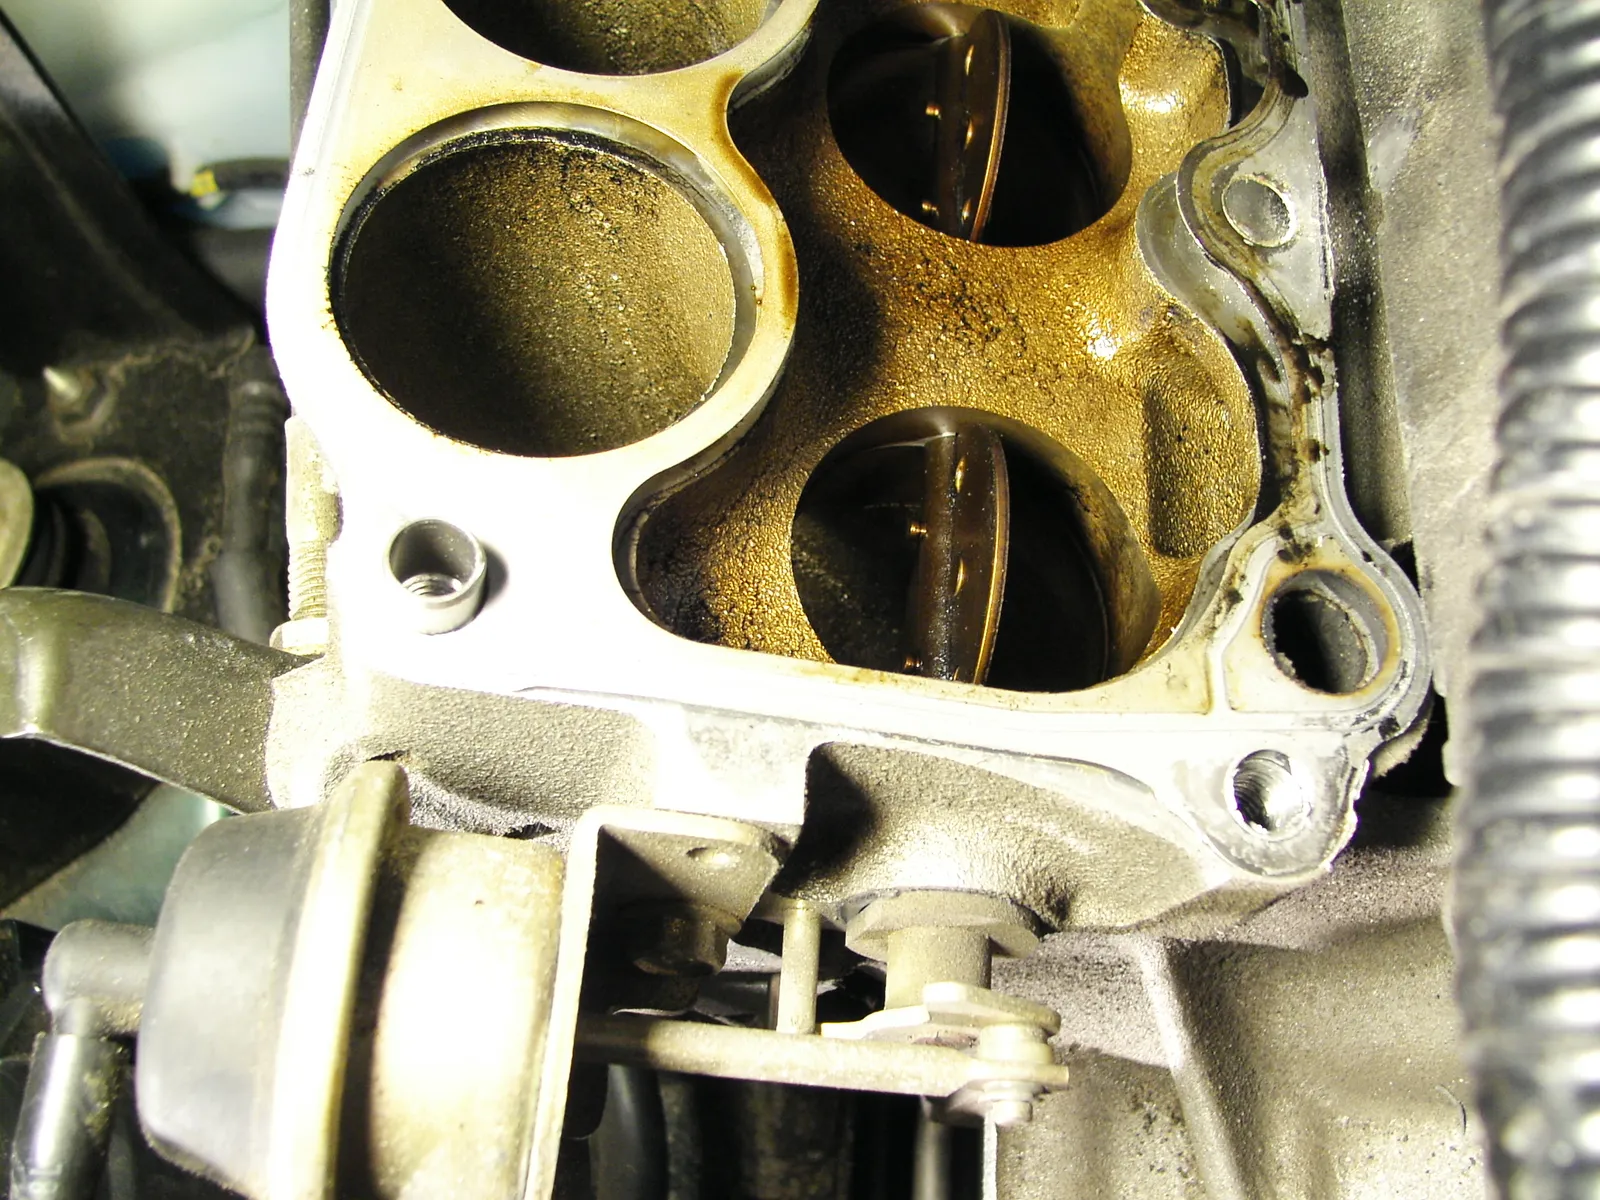
Component Detail
Close-up views of cast components showing surface finish, dimensional features, and application-ready quality.
Aluminum can be die cast or investment cast. KastMfg supplies both routes. Aluminum investment casting is the right choice when geometry is too complex for a two-piece die, annual volume is below HPDC crossover, or you need A356/C355 properties with T6 heat treatment on a part that would blister if die cast with high porosity.
Above roughly 10,000 pieces per year, most aluminum programs migrate to aluminum die casting for unit cost. Below that line, investment casting often wins on total landed cost.
Common Aluminum Investment Alloys
| Alloy | Notes | Applications |
|---|---|---|
| A356 | Good castability; T6 available | Structural, aerospace-style prototypes |
| C355 | Higher strength heat-treated | Brackets, housings, impellers |
| A357 | Higher strength variant | Performance structural |
For high-volume ADC12/A380 programs, see ADC12 vs A380 and custom die casting.
Investment Cast Aluminum vs HPDC
| Investment cast Al | Aluminum die casting | |
|---|---|---|
| Tooling cost | Lower (wax die) | Higher (H13 die) |
| Wall thickness | ~1.5-2.5 mm typical min | ~0.8-1.2 mm achievable |
| Porosity | Lower; T6 feasible | Higher; T6 risky without vacuum |
| Unit cost at 50k/yr | Higher | Lower |
| Complex internal cores | Yes | Limited |
Crossover analysis: die casting vs investment casting.
When We Recommend Each Process
Specify aluminum investment casting when:
- Annual quantity is under ~5,000-10,000 pieces
- Part has internal passages or zero-draft features
- You need T6 heat treat on a complex shape
- Program is prototype or bridge production before die casting tooling
Specify die casting when:
- Volume supports tooling amortization
- Thin walls and tight CT tolerances drive cost
- Surface must be Ra 1.6-3.2 um as-cast for cosmetic plating
Related Pages
- Investment casting
- Lost wax casting
- High pressure die casting
- Gravity die casting - permanent mold alternative
- Aluminum casting guide
Aluminum process selection: casting@kastdiecast.com | +86 138 1403 4409 | No.6, Rungu Road, Nanjing, China
Image credits: Rosebudz92, CC BY-SA 4.0, via Wikimedia Commons; epinkert, CC BY 3.0, via Wikimedia Commons.


Related Resources
Next steps for aluminum investment casting
Lost Wax Casting - Investment Casting Process Explained
Lost wax casting (investment casting) process, tolerances, alloys, and volume economics. When lost-wax precision casting beats die casting for steel, stainless, and complex geometry.
ServiceInvestment Casting Manufacturer - Lost-Wax Precision Parts
Investment casting (lost-wax) for steel, stainless, aluminum, and bronze parts: wax tooling, ceramic shell, heat treatment, CNC, and PPAP for OEM programs from 100 to 10,000+ pieces per year.
ToolingDie Casting Tooling
Understand tool build timing, cavity strategy, and how tooling decisions affect unit cost.
CapabilityQuality Control
Review inspection workflow, traceability support, and process control standards before launch.
Process GuideDie Casting Process
See how casting, trimming, machining, finishing, and inspection fit together in production.
Next StepRequest a Quote
Send your drawing package and target volume to get an engineering-backed quotation.
Need a Quote for Your Project?
Our engineering team is ready to review your requirements and provide competitive pricing with fast turnaround.
Request a Quote